Shop Primer
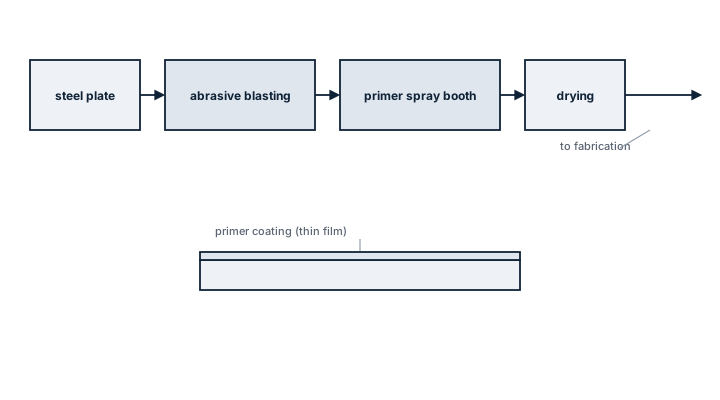
Shop primer is a thin, fast-drying coating applied to steel plate immediately after blasting, before fabrication, purely to hold off flash rust during construction -- it is not the corrosion protection the finished structure will rely on in service.
What to check on a Shop Primer.
1 models from Carboline in Shop Primer. Below: the full model list.
What sets this coating apart
Shop primer has one narrow job: keep freshly blasted steel plate from flash-rusting between the blast booth and the next production step, whether that is cutting, welding or forming. It is applied in seconds by automated spray lines at the steel stockyard or fabrication shop, at a thickness measured in tens of microns, and it is not the coating system the finished hull or tank will rely on for corrosion protection over its service life. That distinction matters because shop primer is formulated to burn away cleanly during welding without generating excessive fumes or porosity in the weld, a requirement that a full corrosion-protection primer is not designed around.
Main components
Binder system
Zinc silicate (inorganic) and zinc epoxy (organic) are the two common families; zinc silicate is more widely used because it welds and cuts more cleanly and resists overcoat lifting better during fabrication.
Zinc content
High metallic zinc loading gives the primer its temporary cathodic protection against flash rust, similar in principle to a full zinc-rich primer but applied at a fraction of the thickness.
Read the full guide
Fast-cure formulation
Solvent balance and cure chemistry are tuned for the seconds-to-minutes throughput of an automated blast-and-prime line, not the longer cure schedules typical of finish coats.
Selection and sizing
Dry film thickness is kept low, generally in the range of 15 to 25 microns, enough to hold off flash rust for weeks to a few months in a covered stockyard but deliberately not a full barrier coating. Compatibility with the intended overcoat system is the real selection criterion: a shop primer must not react badly with the epoxy or coal tar epoxy topcoats that will go over it later in the newbuilding or repair sequence, and it must not generate weld porosity when steel is cut or welded through it.
Typical faults
- Overcoat lifting or intercoat adhesion failure -- an incompatible topcoat applied over aged or contaminated shop primer; the consequence is blistering or peeling of the full coating system, sometimes not visible until the ship is in service.
- Weld porosity from excessive primer thickness -- shop primer applied too thick where a weld will pass through it; the consequence is defective welds that fail inspection or, worse, are missed and weaken the joint.
- Extended exposure before overcoating -- steel sitting primed but uncoated for longer than the primer's protective window; the consequence is flash rust breaking through and requiring reblasting before the finish system can go on.
- Zinc silicate primer in the wrong weld process -- some welding processes are more sensitive to zinc fume than others; the consequence is fume levels that require extra ventilation precautions for welders.
What to look for in a supplier
- Documented compatibility with the specific topcoat system the yard or owner intends to apply, not a generic compatibility claim.
- Weldability and cutting data confirming acceptable fume and porosity behaviour for the fabrication processes actually used.
- Consistent dry film thickness control suited to automated line application, since an uneven film undermines both the flash-rust protection and the later overcoat.
- A realistic protective exposure window stated for the stockyard conditions, humidity and coastal versus inland storage, rather than a single generic figure.
Never treat shop primer as the finished corrosion protection during a yard delay -- steel sitting past its primer's protective window needs reblasting, and skipping that step to save time is a false economy that shows up as coating failure years later.
Models in this type.
The best-documented model of each manufacturer first, then the next — 1 of 1 models in Shop Primer. Every row links to full specifications, documents and service notes.
Manufacturers.
All 24 manufacturers with models of Shop Primer. Names with a manufacturer page open it; the others open a search across the full library.
All manufacturersAlso in Paint & Coating Systems.
The other equipment types in this category.
One request. A person reads it and replies by e-mail.
Tell us the manufacturer, the model and what you need — a part, a service call, a second opinion. A person reads every request and replies by e-mail.
No details at hand? A photo of the rating plate or the part is enough — simply attach it to the request.
Three things people ask first.
Is Shop Primer data free?
Yes. Every model page, every guide and every datasheet for this type is readable without an account. An account adds saved searches and requests, nothing is taken away.
My model is missing — what now?
Send us the nameplate. We identify it by hand, add it to the library, and if you need a part or a service, the request is already on our desk.
Can you source a Shop Primer part?
Yes. Tell us the manufacturer, the model and what you need — a person reads every request and replies by e-mail.